tel:+8613653178029 email:global@xjy8.com whatsapp:8619948472612,8619948472611,8613653178029
Ash Receptacle manufacturer
Vetting Ash Receptacle Manufacturers for Certified Industrial Safety Standards
Trust matters when you pick a safety equipment partner for your site. Every smoking point on the grounds must hold up under the hard demands of a big construction project. On the buying side, you need a clear picture of how long the materials last. See how the factory runs its quality checks too. That way long-term operating risk stays under control.
Unit price alone tells you very little when you pick an industrial supplier. You also have to check whether an Ash Receptacle manufacturer really owns the technical setup to support occupational health management at scale. Plenty of procurement managers struggle to tell a trading company from an actual production plant. That gap raises fair worries about steady fire-containment performance and a supply chain that holds up. Get the manufacturing process wrong in a high-stakes place, such as a North American construction zone or a European industrial site, and you end up with non-compliant industrial safety equipment. Site integrity and safety protocols both suffer.
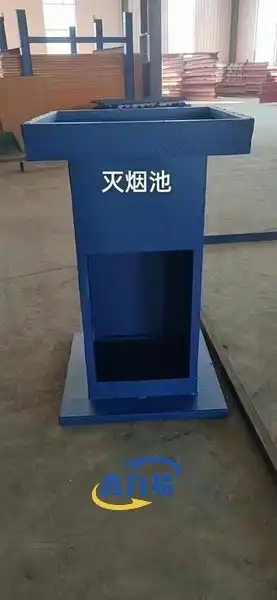
Hebei Xinjiuyi Construction Technology Co., Ltd. answers those worries with fire-safe containment systems built for civilized construction layouts. Every unit comes with a fixed design, so it sits stable near high-risk spots like woodworking sheds and paint storage rooms. Fire hazards drop away, and cigarettes no longer get tossed just anywhere. A special drainage and dust accumulation design keeps daily upkeep simple and worry-free at centralized smoking points. This kind of focused engineering backs up strict occupational health management. It gives offices and living areas a dependable answer for fixed-point smoking control.
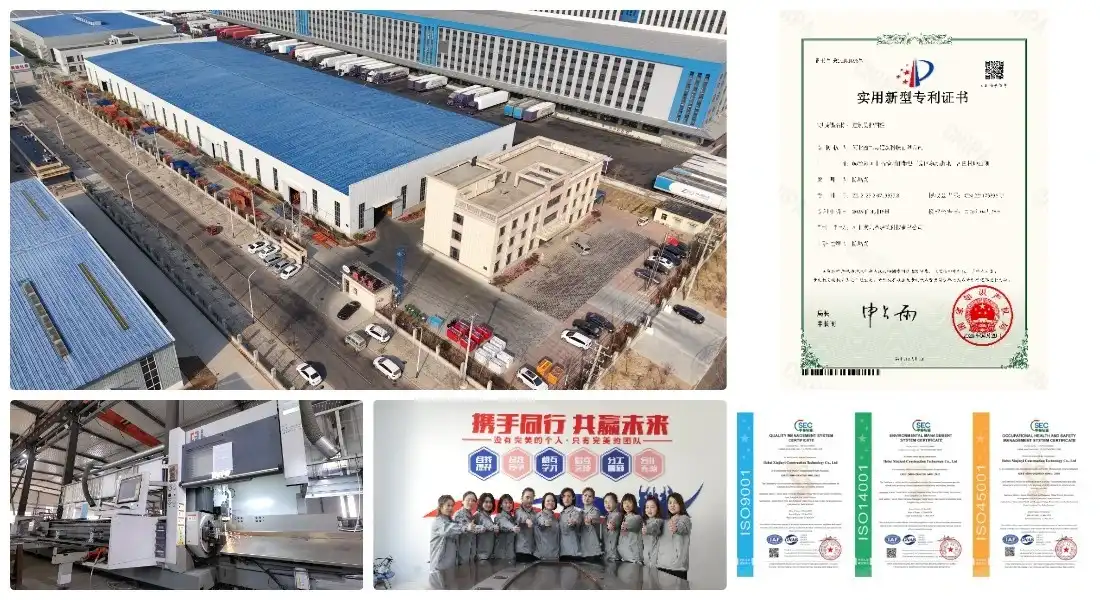
The plant works as a dedicated manufacturer under a strict quality management framework. Certifications ISO9001, ISO45001, and ISO14027 support international compliance. Production capacity leaves room for hard testing of thermal management and oxygen-restricting mechanisms. Every Ash Receptacle that leaves the line meets the environmental and safety expectations of the Australian and New Zealand markets. Material longevity and structural integrity come first on the production lines. Harsh industrial climates put these units through heavy-duty use. Long-term durability and compliance follow. Large-scale industrial safety infrastructure needs that.
A Certified Global Powerhouse in Ash Receptacle Manufacturing Excellence
Hebei Xinjiuyi Construction Technology Co., Ltd. is a leading manufacturer of industrial grade Ash Receptacle products. We supply verified Ash Receptacle manufacturer products to safety markets with the toughest demands. A manufacturing history of more than 10 years stands behind us. Our site can export over 50,000 units a year. Shipments go to North America. They also go to Europe. Australia and New Zealand receive them too. We are a real manufacturer. That comes from our large physical plant and direct control of the whole production process. Every international partner can see how the work is done.
Our technical work centers on fire safe containment systems. These systems are built specifically for high risk industrial environments. We use advanced stable placement designs and our own drainage systems. Maintenance gets easier. Maximum durability holds up in extreme outdoor conditions. Our facilities fully comply with ISO 9001 for quality management. They also comply with ISO 45001 for occupational health and safety. The strict ISO 14027 environmental standards are part of this commitment. This triple certified approach means every Ash Receptacle we make meets the civilized construction requirements of top tier international contractors and safety officers.
Today, our products are used in more than 20 countries. They protect critical areas from fire hazards. These areas include woodworking sheds, paint storage rooms, and office complexes. Oxygen starvation baffle systems are part of the design. Fixed point layouts are used too. Together they give a reliable solution. It supports site safety and environmental sanitation. You can verify our manufacturing credentials. Talk with our engineering team about your project requirements. That way your site can meet the highest safety benchmarks.
✅ 10+ Years Manufacturing Power
✅ ISO 9001/45001/14027 Certified
✅ 50,000+ Annual Unit Capacity
✅ Exporting to 20+ Countries
✅ Direct Factory-Source Transparency

Certified Industrial Manufacturing That Meets Fire Safety Rules Worldwide
Buying industrial-grade safety equipment takes more than a seller. You need a partner that can, as an Ash Receptacle manufacturer, hit strict fire-containment standards and handle high-volume demand. Many procurement officers face risk from unverified suppliers. Such suppliers offer non-compliant bins that corrode or fail in harsh construction environments. A vertically integrated manufacturing process closes the gap between safety on paper and durability on site. It makes sure every unit carries superior oxygen-starvation technology. High-performance materials and special drainage systems keep operation maintenance-free across different climate zones.
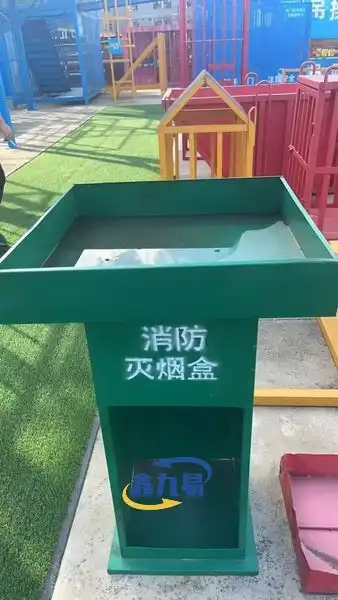
- Exact Fire Containment and Oxygen-Starvation Engineering
- Engineering teams work to remove fire hazards at the source. They use special internal baffle systems that put out cigarette butts on their own. No sand or water is needed. These designs control airflow and stop smoldering fires in high-risk zones. Examples include woodworking sheds and paint storage rooms. Each unit is built to handle industrial use. It also keeps occupational health standards and site cleanliness in place.
- View Engineering Specs
- Heavy-Duty Manufacturing for Industrial Use
- The factory makes receptacles from heavy-duty galvanized steel and UV-stabilized coatings. These units are built for the harshest outdoor conditions in North America and Europe. A fixed-point design keeps them stable at construction sites. Drainage and dust accumulation features are built in. Daily upkeep gets easier because of them. In demanding environments, those features cut down on maintenance work.
- How the Manufacturing Process Works
- Strict Checks on Quality and Safety
- Authenticity gets proven by a full quality process. Salt spray testing is one part. Coating adhesion is checked. Structural load assessments are done too. Each batch goes through fire-rating validation. That step confirms the product meets international safety codes. Environmental regulations are covered as well. Receptacles used in offices or living quarters get detailed inspections. Those checks keep performance consistent.
- Download Quality Reports
- Scalable Production for Global Project Fulfillment
- Major infrastructure projects need a manufacturer that can handle bulk orders. Lead times for clients in Australia and New Zealand still have to hold. Vertically integrated facilities run the whole lifecycle. Raw material sourcing is the start. Final logistics is the end. Deployment runs smoothly. Logistics networks support fast deployment. They serve civilized construction initiatives around the world.
- Check Supply Capacity
15,000+ | Monthly Production Capacity
500+ Hours | Salt Spray Corrosion Resistance
24-Hour | Rapid Prototype Development Cycle
100% | Fire-Safe Certification Compliance
FAQs
1. What is your typical manufacturing lead time and minimum order quantity (MOQ) for bulk orders?
Our standard manufacturing lead time for bulk orders is 15 to 25 business days, depending on the specific volume and customization requirements. To support professional distributors and facility managers, we maintain a flexible minimum order quantity, typically starting at 50 units for standard designs. This timeframe includes our rigorous multi-stage quality check to ensure every unit meets fire safety protocols. For urgent construction site requirements in North America or Australia, we can often provide expedited production schedules. Contact our sales team today to receive a precise quote and production timeline tailored to your project’s scale.2. Can you provide factory-level customization for our specific industrial safety and branding requirements?
Yes, we offer comprehensive OEM and ODM services, allowing you to customize the color, dimensions, and branding of each Ash Receptacle to align with your corporate identity or site safety codes. We utilize a high-precision UV-stabilized powder coating process that can match any RAL color code, ensuring the finish remains durable in harsh outdoor environments. With over 10 years of experience in the manufacturing sector, our engineering team can also modify the internal baffle systems to meet specific fire-restriction needs. Please submit your design specifications or logo files to our technical department for a free prototype evaluation.3. How do I verify the quality management standards and safety certifications of your production facility?
You can verify our manufacturing strength through our comprehensive certification portfolio, which includes ISO9001 for quality management, ISO45001 for occupational health and safety, and ISO14027 for environmental standards. Our facility undergoes annual third-party audits to ensure compliance with global safety regulations. Every Ash Receptacle we produce is subjected to an oxygen-restriction test, ensuring lit materials are extinguished in under 60 seconds, and 500+ hours of salt spray testing to guarantee corrosion resistance. We invite potential partners to conduct a virtual factory tour or request our certified test reports to validate our production integrity before placing an order.4. Do you have the capacity to handle large-scale supply chains for North American and European distributors?
We currently manage a robust supply chain that exports high-durability safety equipment to over 30 countries, including dedicated logistics support for North America, Europe, and New Zealand. Our factory is equipped with automated welding and coating lines that allow for a monthly output of over 10,000 units, ensuring we can meet the demands of large-scale construction or municipal projects without delay. We are familiar with ASTM B117 standards and international shipping regulations, providing all necessary customs documentation for a seamless transition. You can view our recent case studies to see how we have successfully scaled production for global safety equipment providers.5. What are the key criteria for selecting a reliable Ash Receptacle manufacturer for high-risk industrial sites?
Evaluating a manufacturer for high-risk environments requires a focus on material grade, fire-containment technology, and certified management systems. A reliable supplier should utilize 304 or 316-grade stainless steel or heavy-duty galvanized steel to ensure structural integrity under extreme heat. Furthermore, verify that the manufacturer employs an "oxygen-starvation" design rather than relying on sand or water for extinguishment. Professional manufacturers must hold valid ISO certifications and provide transparent data on thermal management and coating adhesion (ISO 2409). Choosing a supplier with a proven track record in manufacturing for the construction and woodworking industries ensures the equipment will withstand rigorous daily maintenance and high-frequency use.
Best Selling Products
Related Blogs
Related Search
tel:+8613653178029 email:global@xjy8.com whatsapp:8619948472612,8619948472611,8613653178029